Home › Capabilities › 3+2 Axis CNC Machining
3+2 Axis CNC Machining for Aluminum Parts
30 of CHX Metal's 100 five-axis machining centers run the 3+2 configuration, cutting aluminum parts on five faces in a single setup at ±0.005 mm. The plant holds 220 machines across 5,000 m2 and ISO 9001:2015, with prototypes in 3-7 days and production in 7-15 days from 1 piece.
What 3+2 Machining Does Differently
A 3+2 machine is not a weaker five-axis machine. It is a three-axis machine that brings the part to the tool. The three linear axes cut as they always do; the two rotary axes index the table to a known angle and lock, so each face is machined with the stiffness of a straight three-axis cut. The difference from simultaneous five-axis is the locked table: no continuous interpolation, no dynamic error stacking while the rotary axes move.
For prismatic aluminum parts, that trade is usually the right one. A housing with machined faces on the front, back, top, bottom and one side needs five setups on a three-axis machine, and every re-clamp adds position error. On a 3+2 machine the same part is cut in one setup: index to +90°, machine; index to −90°, machine; index to 45° for the chamfer, machine. Bores that must stay concentric, and faces that must stay parallel, are cut without ever releasing the part.
The limits are equally clear. Deep contoured cavities, twisted blades and free-form surfaces with continuous curvature still belong on a simultaneous five-axis machine. Where a part needs a true swept surface, we move it to the simultaneous centres rather than force it onto a 3+2 table.
Why Aluminum Is the Natural Fit
Aluminum rewards exactly what 3+2 does well. The metal cuts fast, so the cost of a part is dominated by handling and setup, not by spindle time. Removing four re-clamps from a five-face housing removes most of the handling, and with it most of the scrap risk. Aluminum also moves under clamping load; a part clamped once and machined on five faces keeps its geometry, while the same part re-clamped four times accumulates the distortion of four separate grips.
Chip evacuation is the second reason. Aluminum produces large, soft chips that pack into pockets and recut under the tool. Indexing the table lets the open face point down or sideways so chips fall away, and we run through-spindle coolant on the deep pocket work to keep the cut stable. Thin walls between 1.0 mm and 2.0 mm are cut in multiple light passes with the part supported by the fixture rather than by the wall itself.
We machine aluminum 6061-T6 for housings, brackets and heat-sink bodies, 7075-T6 where strength matters more than anodizing uniformity, and 5083 for welded assemblies. Hard anodizing, clear or black anodizing, chromate conversion coating, bead blasting and laser marking are all handled in-house or through qualified local finishing partners, with the finish specified on the drawing rather than guessed at shipment.
30 of 100 Five-Axis Centres Run 3+2
CHX Metal operates 220 machines: 100 five-axis machining centers, 50 CNC lathes and 70 Swiss-type automatic lathes. Thirty of the five-axis centers are set up for 3+2 positional work and are the ones we schedule aluminum housings, plates and brackets onto. The working envelope on those centers reaches 1000 × 600 × 500 mm, which covers most enclosure and chassis work without splitting a part across two setups.
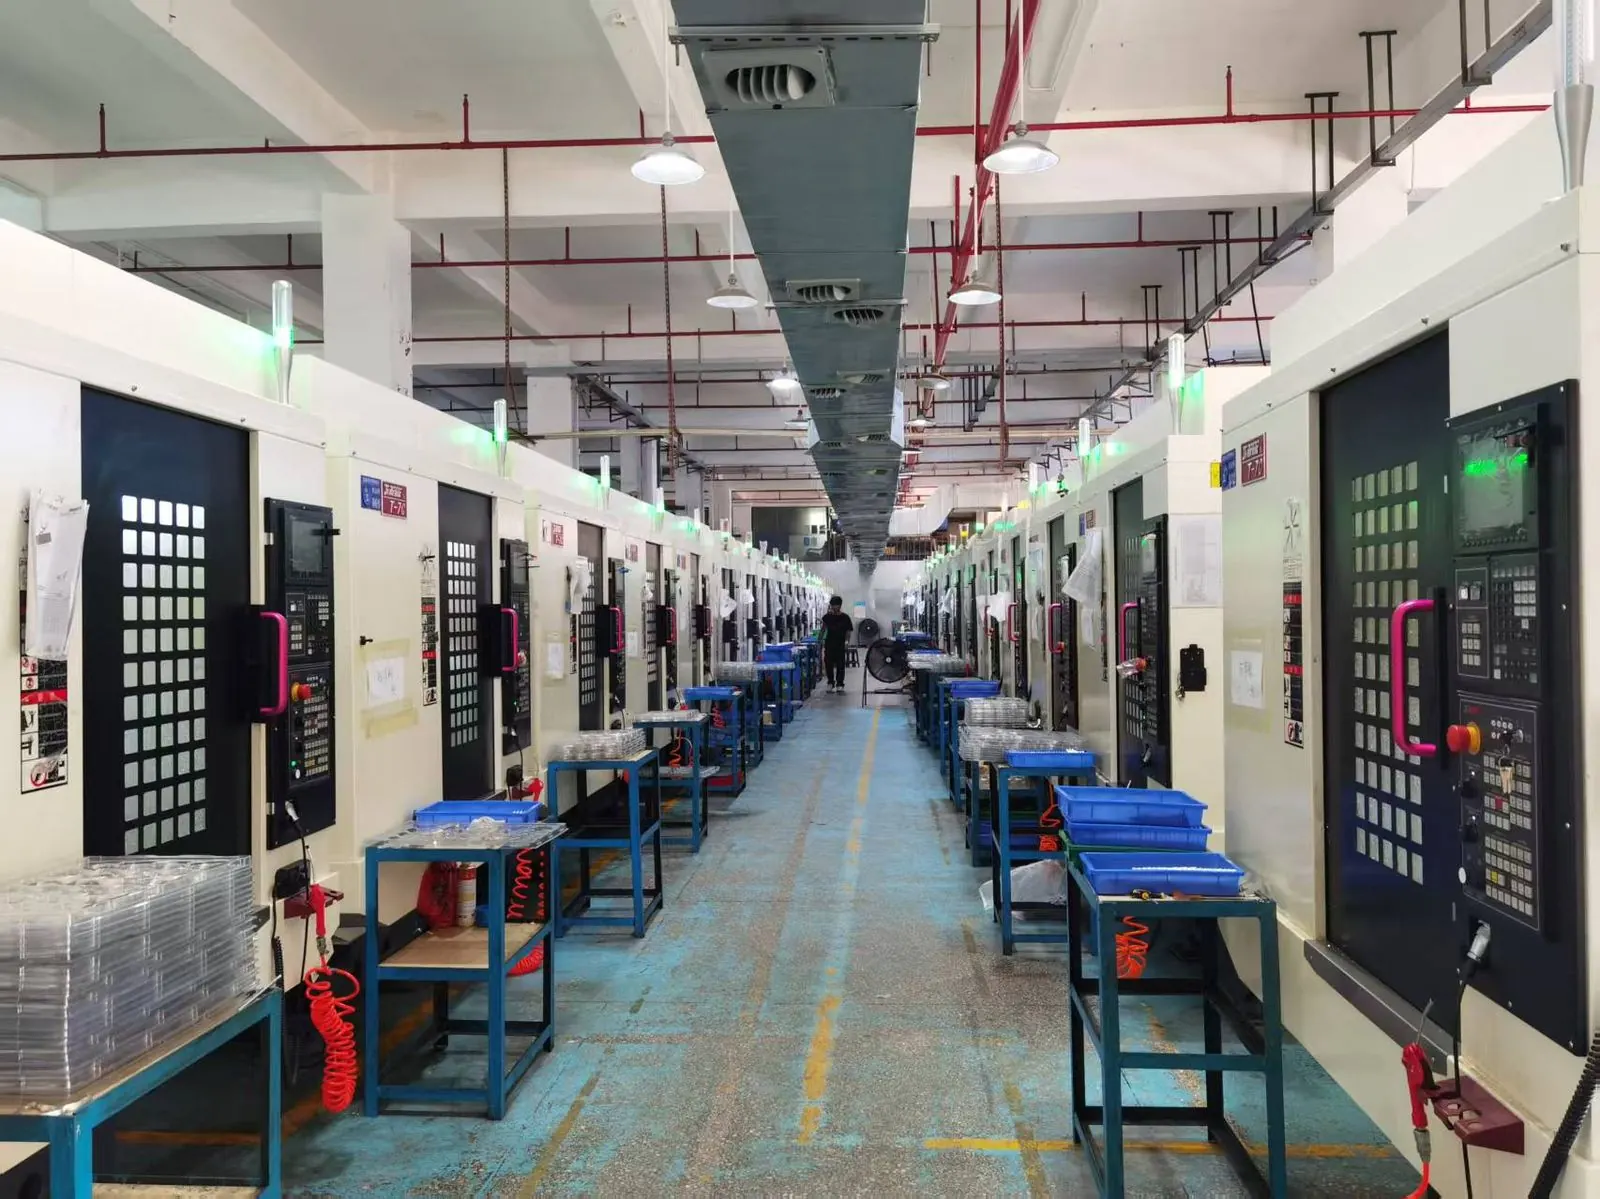
Keeping a dedicated 3+2 pool matters for scheduling. Parts that need positional work do not queue behind simultaneous five-axis jobs, and the fixtures for a repeat family stay mounted between batches. Repeat orders in the 50 to 5,000 piece range run on the same machines with the same fixture offset, which is why the second order usually measures the same as the first.
Parts We Run on 3+2 Centres
- Aluminum enclosures and housings — five faces machined in one setup, bores and faces held in the same tolerance band.
- Heat sinks and liquid-cooling plates — fin arrays on one face, mounting and port faces on the others, no re-clamp between them.
- Robot joints and end-effector bodies — bearing bores on two perpendicular faces, cut without releasing the part.
- Optical benches and module housings — flatness and perpendicularity carried across faces, critical where an optical axis has to stay true after assembly.
- UAV frames and automation brackets — thin-wall aluminum structure with pockets on multiple faces.
- Semiconductor and test fixtures — plate work with pockets, slots and dowel holes referenced to one datum.
3-Axis vs 3+2 vs Simultaneous Five-Axis
| Criterion | 3-axis | 3+2 (positional) | Simultaneous 5-axis |
|---|---|---|---|
| Setups for a five-face part | 5 or more | 1 | 1 |
| Rigidity at the cut | Highest | High, table locked | Lower, rotary axes live |
| Angular position error | Accumulates per setup | Fixed by index | Continuous, stack-up in motion |
| Best for | Single-face plate work | Prismatic multi-face parts | Contoured surfaces, impellers |
| Cost per part | Lowest for simple parts | Lowest for five-face parts | Highest, justified by geometry |
From Drawing to Shipment
Every drawing is reviewed by a CAM engineer before quoting. The review returns within 24 hours and covers what the part needs: whether a tolerance is tighter than the process can hold, whether a corner needs a smaller tool than the pocket allows, whether a wall will deflect, and where the datum should sit so that inspection means something. That feedback arrives with the price, not after the order.
Prototypes ship in 3-7 days and production runs in 7-15 days, from 1 piece. First article inspection is mandatory on every new part number: critical dimensions are measured on a CMM, recorded, and shipped with the parts as a dimensional report. For production orders we track the same dimensions across the batch so that a trend shows up before a part goes out of tolerance.
The plant runs ISO 9001:2015 (NOA198428) and ISO 14001:2015 (NOA2100184), covers 5,000 m2 with more than 100 staff, and ships export orders with the paperwork buyers actually need: material certificates, finish certificates, dimensional reports and country-of-origin documentation.
Frequently Asked Questions
What is 3+2 axis CNC machining?
Three linear axes plus two rotary axes that index to a fixed angle and lock. The part is machined on five faces in one setup, with three-axis rigidity at every indexed position.
How many 3+2 machines does CHX Metal run?
Thirty of our 100 five-axis machining centers are configured for 3+2 positional work; the rest run simultaneous five-axis.
Which aluminum grades do you machine?
6061-T6 for housings and brackets, 7075-T6 for high-strength structural parts, 5083 for welded assemblies. Other grades quoted on request.
What tolerance can you hold on aluminum?
±0.005 mm on critical features, verified on a CMM, with five-face work keeping bore-to-bore relationships inside the same band.
What is the lead time?
Feedback in 24 hours, prototypes in 3-7 days, production in 7-15 days, minimum order 1 piece.
Send a drawing, get a 3+2 quote in 24 hours
Email: mc@chxmetal.com
WhatsApp: +86-181-3885-0989
Related Capabilities
- 5 axis CNC machining in China — simultaneous five-axis for contoured parts
- 5-axis aluminum CNC machining — aluminum-specific five-axis work
- CNC aluminum parts — material and finish options
- Precision aluminum CNC machining — tight-tolerance aluminum work
- Aluminum housing CNC machining — enclosure and housing families
- Small batch aluminum housings — low-volume runs from 1 piece
- CNC machining services — turning, milling and drilling
- Surface treatment — anodizing, plating and coating
- CNC machining cost guide — what drives the price per part
- CNC machining quote from China — how to compare quotes
- Simultaneous vs 3+2 five-axis — which suits your part
- Humanoid robot parts — joints, end effectors and finger parts
Engineering notes: Simultaneous 5-Axis vs 3+2: Which Does Your Part Need?